
Circular vibrating screenIt is a crucial piece of screening equipment used to separate granules, powders, minerals, aggregates, construction chemicals, and various bulk materials based on particle size. A properly functioning circular vibrating screen within a production line enhances product quality, balances capacity, and ensures greater stability in downstream processes. However, when blinding (clogging) occurs on the screen surface, production efficiency drops rapidly. Material fails to pass through the screen apertures and accumulates on top; the feed flow is disrupted, and the plant fails to achieve its target capacity. Therefore, blinding in circular vibrating screens is not merely a minor maintenance issue; it represents a technical loss of efficiency that impacts the entire production line.
Metkan Makine, Crushing and screening systems, micronized crushing and screening lines, construction chemicals facilities and industrial conveying solutions ...evaluates screening performance at the heart of the process during development. This is because if the screen is not selected correctly, the crusher, conveyor, bucket elevator, mixer, and bagging line are also affected by this inefficiency. Clogging in circular vibrating screens The problem often results from wet material, an incorrect screen aperture, overfeeding, insufficient vibration, worn screen mesh, an incorrect inclination or inadequate maintenance. In this article, we examine in detail the 7 technical causes that reduce screening efficiency and explain the appropriate solutions.
Contents
- What is clogging in circular vibrating screens?
- How does clogging in circular vibrating screens affect the production line?
- Do moist and sticky materials cause clogging?
- How does an incorrect screen aperture size reduce screening efficiency?
- Why does overfeeding cause clogging?
- How do vibration settings affect the performance of circular vibrating screens?
- What problems arise from worn or damaged screen mesh?
- What are the issues regarding incorrect screen inclination and installation errors?
- Do a lack of maintenance and cleaning issues increase clogging?
- How can clogging in circular vibrating screens be prevented?
- Metkan Makine circular vibrating screen solutions
- Frequently Asked Questions
What is blinding in circular vibrating screens?
Clogging in circular vibrating screensIt is a condition where material fails to pass regularly through the apertures of the screen surface and instead accumulates on the screen. This problem arises due to a mismatch between the product particle size and the screen aperture, the material's moisture content, the feed rate, or vibration settings. When the screen surface becomes blinded, material flow slows down, and screening capacity drops. Furthermore, product classification is compromised; fine particles fail to pass into the intended fraction and remain with the coarse product. This situation complicates quality control processes and increases the circulating load within the production line. Therefore, blinding in circular vibrating screensit is a technical issue that directly affects product standards.
However, blinding is not always easily visible to the naked eye. In some facilities, the screen does not become completely blocked; instead, efficiency gradually declines as a significant portion of the apertures becomes filled. Operators often detect this issue through reduced capacity, material buildup on the screen, motor strain, or fluctuations in product quality. Additionally, a blinded screen surface cannot utilize vibration energy efficiently, resulting in lower screening performance for the same energy consumption. At this stage, the operation should not merely clean the screen mesh but must identify the root technical cause of the blinding.
How does blinding in circular vibrating screens affect the production line?
Clogging in circular vibrating screensIt directly reduces the capacity of the production line. When the screen surface fails to perform its function effectively, material classification slows down, and the process flow becomes congested. In crushing and screening plants, this prevents the product discharged from the crusher from being separated into the correct fractions. Construction chemicals In production processes, it hinders the flow of powdered or granular raw materials at the desired particle size distribution. Furthermore, fine products unable to pass through the screen due to clogging may end up in the recirculation line. This results in unnecessary reprocessing and increased energy consumption. Consequently, clogging creates a bottleneck that affects not only screen performance but the entire production line.
Clogging also negatively impacts equipment lifespan. Material accumulation on the screen surface increases the weight load, placing greater strain on the vibration mechanism. This process imposes extra stress on bearings, springs, the motor, and the chassis. Additionally, uneven material distribution causes localized wear on the screen surface. If the production team fails to resolve the issue promptly, maintenance costs rise, and the risk of unplanned downtime increases. Therefore, facilities should not view clogging in circular vibrating screens merely as a cleaning issue. The correct approach requires a holistic evaluation of material properties, screen selection, feed patterns, and maintenance schedules.
1. Do Damp and Sticky Materials Cause Clogging?
Moist and sticky materials are among the most common causes of clogging in circular vibrating screens.When material absorbs moisture, particle surfaces adhere to one another, and flowability decreases. Consequently, the product does not spread easily across the screen apertures. Fine particles become lodged within the openings, eventually blinding the screen surface. This problem frequently occurs with high-clay-content aggregates, damp sand, certain mineral mixtures, raw materials for construction chemicals, and powdered products prone to agglomeration. As moisture levels rise, a layer of material forms on the screen. This layer diminishes the separation effect of the vibration and reduces screening efficiency.
Furthermore, sticky material does not merely clog the screen apertures; it also creates an uneven load on the screen surface. Circular vibrating screenVibrating screens utilize vibrational energy to advance material across the surface and separate it according to particle size. However, when sticky product adheres to the surface, this movement is impeded. Material flow slows down, accumulation increases at the feed end, and an unbalanced product distribution occurs at the discharge end. Therefore, operators should review raw material storage conditions, feed rates, and screen aperture sizes before screening moist products. Additionally, where necessary, more suitable screen media, different surface structures, or pre-drying methods should be employed.
2. How Does an Incorrect Screen Aperture Size Reduce Screening Efficiency?
Incorrect screen aperture size, the most critical selection factor that increases clogging in a circular vibrating screen in circular vibrating screens. The screen aperture must be determined based on the material's particle size, the target product fraction, and the production capacity. If the aperture is selected to be smaller than necessary, material passage becomes difficult, and fine particles get trapped in the openings. The problem of "blinding" (or pegging) intensifies, particularly when the screen aperture and the material particle size are very close to each other. This causes the screen surface to become blocked quickly. Furthermore, when the operator increases the feed rate to maintain capacity, clogging accelerates. Consequently, product quality and hourly production output decline.
On the other hand, a screen aperture that is larger than necessary also leads to quality issues. In this case, unwanted coarse particles mix into the undersize fraction, compromising product standards. Therefore, selecting a screen does not simply mean choosing a wide aperture to prevent clogging. The correct choice requires a balanced engineering calculation between product quality and capacity. Metkan Makine...evaluates material characteristics, target product size, and line capacity together in circular vibrating screen solutions. This aligns the screen aperture with production goals. Through this approach, the operation reduces the risk of clogging while maintaining more stable product quality.
3. Why Does Excessive Feeding Cause Clogging?
Excessive feeding blinding in circular vibrating screens is a significant factor that rapidly exacerbates the problem. The screen surface is designed to efficiently handle a specific material load. When the feed rate exceeds this capacity, the material does not spread evenly across the screen surface. A thick layer forms, preventing fine particles in the lower layer from reaching the screen apertures. Consequently, the product moves toward the discharge point without undergoing proper screening. Furthermore, the accumulated material on top dampens the vibration; even if the screen operates at the same speed, actual screening performance declines. Therefore, excessive feeding does not necessarily equate to higher production output.
Furthermore, Overfeeding increases mechanical stress. The screen body, springs, motor, and fasteners operate under higher loads. Over time, this degrades vibration characteristics and further exacerbates clogging. Equipment used in the feed line—such as the belt conveyor, screw conveyor, bunker, or bucket elevator must be compatible with the capacity of the circular vibrating screen. If upstream equipment feeds material to the screen without control, the screen surface quickly becomes overloaded and loses efficiency. The production plan should therefore set the feed rate according to the screen capacity. Metkan Makine considers this compatibility during plant integration to achieve a more balanced process flow.
4. How Does Vibration Adjustment Affect Circular Vibrating Screen Performance?
The performance of a circular vibrating screendepends on the correct adjustment of the vibration motion. Vibration intensity, frequency, amplitude, and direction of motion determine the speed at which material moves across the surface and how it passes through the screen. If vibration is insufficient, the material cannot move actively across the screen surface. Consequently, particles fail to orient themselves toward the screen apertures and begin to accumulate on the surface. Insufficient vibration accelerates clogging, particularly with fine-grained or slightly moist products. Furthermore, as the material layer thickens, the screen surface becomes increasingly obstructed. Therefore, a low vibration setting becomes a primary cause of capacity loss.
However, excessive vibration is not the right solution either. Excessive vibration causes material to move across the surface too rapidly, shortening the time available for fine particles to pass through the screen. It also places an excessive load on mechanical components, leading to premature wear on bearings, springs, and connecting parts. Proper vibration settings ensure that material remains on the screen long enough for effective classification. Operators should review vibration characteristics when switching products, as dry aggregate, moist sand, fine dust, and granular construction chemicals do not yield the same efficiency with identical vibration settings. Therefore, adjustments must be made according to specific process conditions.
5. What Problems Do Worn or Damaged Screen Meshes Cause?
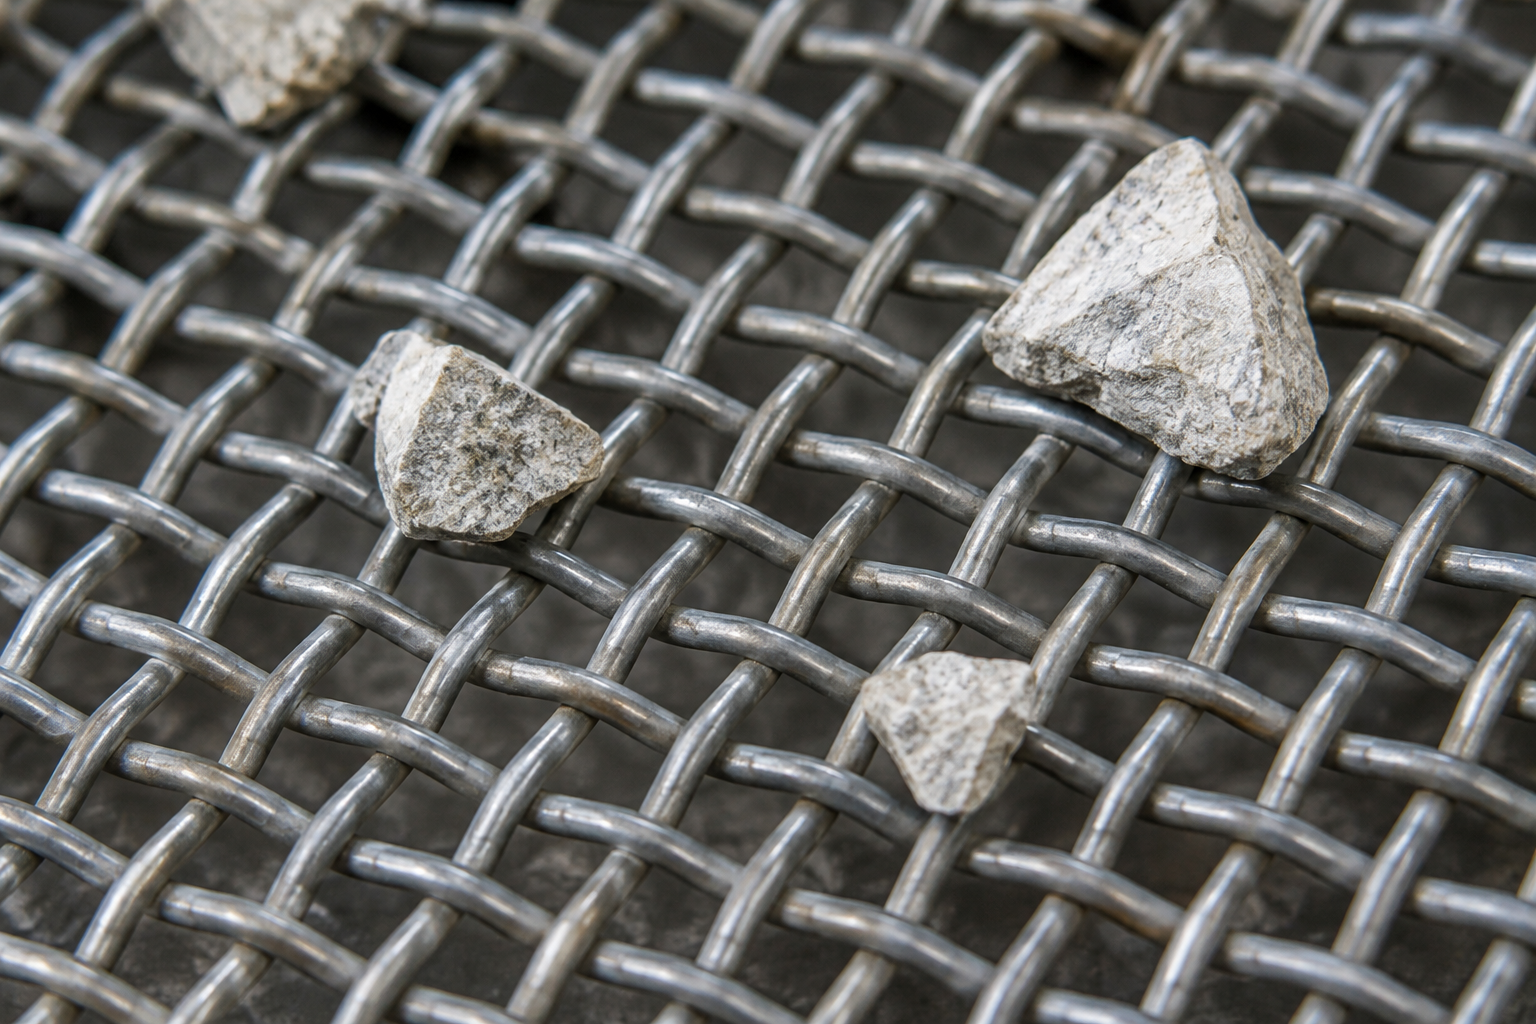
The screen meshis the component of the circular screen that comes into the most intense contact with the product. Therefore, wear, tearing, loosening, or deformation directly affects screening performance. Worn mesh alters the aperture size and disrupts product classification. In some areas, the aperture widens, while in others, passage is restricted due to mesh deformation. This irregularity causes clogging in one section of the screen while allowing unwanted oversized particles to pass through another. Furthermore, a loose screen mesh fails to transmit vibration energy effectively. Consequently, the surface cleaning action is diminished, and material becomes more prone to getting stuck in the mesh openings.
A damaged screen mesh also compromises production reliability. A small tear or localized deformation may seem insignificant at first; however, as production continues, the damage worsens, and product quality falls out of control. Furthermore, loose areas on the screen surface increase material accumulation. Therefore, the maintenance team should inspect the screen mesh at regular intervals, rather than only when a breakage occurs. Wear levels, mounting tension, surface cleanliness, and aperture size should be regularly examined. Proper maintenance reduces blinding and extends the economic lifespan of the screen..
6. What Are Incorrect Screen Inclination and Installation Errors?
Inclination in circular vibrating screensis a critical design parameter that determines the speed at which material moves across the surface. If the inclination is too low, material moves slowly across the surface, leading to a buildup in the feed zone. This accumulation causes the screen apertures to fill up and increases blinding. Conversely, if the inclination is too steep, material moves across the surface too rapidly. In this case, fine particles do not have sufficient time to pass through the screen, resulting in poor product separation. Therefore, the correct inclination must be determined based on material type, particle size distribution, moisture content, and target capacity.
Installation errors also significantly reduce screening efficiency.An unbalanced fit of the screen on the chassis, uneven spring operation, loose connection points, or surface misalignment errors disrupt vibration characteristics. In such cases, the screen surface does not move uniformly, causing material to accumulate in specific areas. Furthermore, improper installation creates unnecessary stress on mechanical components. During initial setup or commissioning following maintenance, the operator must verify vibration, leveling, connections, and feed direction. Metkan Makine considers not only the machine itself but also the operating conditions of the production line during equipment installation. This approach ensures more stable screening performance.
7. Do Lack of Maintenance and Cleaning Issues Increase Clogging?
Lack of maintenance, blinding in circular vibrating screens ...causes the problem to become permanent over time. Material remaining on the screen surface hardens—especially with moist or fine powdery products—and narrows the aperture openings. What initially appears as minor buildup can severely reduce screening capacity if regular cleaning is neglected. Furthermore, failure to regularly inspect springs, bearings, the motor, and connection components disrupts vibration balance. This imbalance prevents the material from moving correctly across the surface. Consequently, clogging stems not only from the screen mesh itself but also from a lack of maintenance across the entire mechanical system.
A regular maintenance planis one of the most effective ways to prevent clogging. Facilities should establish daily, weekly, and monthly checklists based on production intensity. Daily checks should monitor surface buildup, material flow, and any abnormal noises. Weekly checks should inspect the screen mesh, connections, and spring system. Monthly checks should involve a detailed review of the motor, bearings, and chassis connections. Additionally, the screen surface should be cleaned and aperture openings inspected whenever the product type changes. This disciplined approach reduces unplanned downtime and maintains screening efficiency over the long term.
How to Prevent Clogging in Circular Vibrating Screens?
To prevent clogging in circular vibrating screens, material properties must first be accurately analyzed. Moisture content, particle size distribution, density, stickiness, and abrasiveness directly determine screening behavior. If a facility selects screen apertures or vibration settings without considering this data, the risk of clogging increases. Furthermore, the feeding system must operate in alignment with the screen's capacity. Controlled and uniform feeding balances the material layer on the screen surface, allowing fine particles to reach the apertures more easily. Therefore, an operation aiming to reduce clogging must focus not only on the screen surface itself but on the entire flow of material entering the screen.
Secondly, equipment settings must be adjusted according to process conditions. Screen inclination, vibration settings, screen mesh type, and aperture size must be compatible with the material characteristics. These parameters should be re-checked whenever the product changes. Furthermore, overfeeding must be prevented, and the formation of an excessively thick material layer on the screen surface must be avoided. When necessary, pre-screening, bunker adjustments, or the use of alternative feeding equipment can enhance efficiency. Additionally, maintenance and cleaning schedules must not be neglected; regular cleaning keeps screen apertures open, while regular mechanical inspections maintain vibration performance.
Metkan Makine Circular Vibrating Screen Solutions
Metkan Makine Circular vibrating screen systems Crushing and screening plants, micronized screening lines, construction chemicals production and evaluates them according to industrial process requirements. The company views the screen not merely as a standalone machine, but as a critical classification point within the production line. Consequently, factors such as particle structure, moisture content, target capacity, feeding method, and output fractions are analyzed holistically. A proper screen design ensures a more stable flow in the production line. It also reduces the risk of clogging, preserves product quality, and contributes to the more efficient operation of downstream equipment.
Metkan Makine plans crushers, conveyors, bucket elevators, mixers, bagging lines, and automation solutions in conjunction with the performance of the circular vibrating screen, tailored to the facility's specific needs. This approach ensures a balanced capacity, as the selection of incorrect equipment upstream or downstream of the screen can reduce screening efficiency. Particularly in Construction chemicals, mining and aggregate facilities, optimal screening performance directly impacts production standards. If your operation blinding in circular vibrating screensis experiencing capacity drops, product classification issues, or a need for frequent maintenance, Metkan Makine you can contact us to request a technical solution customized for your production line.
Frequently Asked Questions
What is the most common cause of clogging in circular vibrating screens?
Clogging in circular vibrating screens It most frequently occurs with moist and sticky materials, or due to incorrect screen aperture settings and overfeeding. Insufficient vibration settings and a lack of maintenance also exacerbate clogging. To find the right solution, the operation must evaluate material properties and equipment settings together.
What happens if the screen aperture is too small?
When the screen aperture is selected to be smaller than necessary, material passage becomes difficult, and particles get trapped in the openings. This causes the screen surface to blind (clog) quickly. Additionally, capacity drops, and product classification is compromised.
Why does overfeeding reduce screening efficiency?
Overfeeding creates a thick layer of material on the screen surface. This layer prevents fine particles from reaching the screen openings. It also dampens the vibration movement and reduces screening performance.
How can screen clogging be reduced with moist materials?
To reduce clogging with moist materials, the feed rate must be controlled, the appropriate screen aperture selected, and the screen surface cleaned regularly. Furthermore, material storage conditions should be improved, and agglomeration minimized. If necessary, a different screen wire configuration should be chosen.
Does increasing the vibration setting improve screening efficiency?
Increasing the vibration setting does not always improve efficiency. Excessive vibration causes the material to move across the surface too quickly, reducing the time available for fine particles to pass through the screen. The correct vibration setting should be determined based on the material type and target capacity.
When should the screen mesh be replaced?
The screen mesh should be replaced when it becomes worn, loose, or torn, or when the aperture openings become deformed. Additionally, the mesh should be inspected if fluctuations in product quality or a drop in capacity are observed. Regular maintenance reduces unplanned downtime.
What checks should be performed during circular vibrating screen maintenance?
During maintenance of the circular vibrating screen, the screen mesh, springs, bearings, motor connections, frame connections, and surface cleanliness should be inspected. Additionally, the feed arrangement and product flow should be observed. These checks maintain screening efficiency and reduce the risk of clogging.
In which facilities are Metkan Makine's circular vibrating screen solutions used?
Metkan Makine Circular vibrating screen solutions; Crushing and screening plants, construction chemicals lines, micronized production facilities, mining and aggregate are used in these processes. The company develops suitable screening solutions based on product characteristics and capacity targets.
Properly Analyze Clogging Issues in Circular Vibrating Screens
Clogging in circular vibrating screens reduces production capacity, compromises product quality, and increases maintenance costs. You can significantly mitigate this problem through proper screen selection, controlled feeding, appropriate vibration settings, and regular maintenance.
Metkan Makine evaluates your production line holistically, offering circular vibrating screens, crushing and screening systems, construction chemical plants, conveyor lines, bagging systems, and automation solutions. To enhance screening efficiency and ensure more stable production at your facility... Metkan Makine with contact us.


